How to Choose the Right Polyester Fiber for Your Business?
Choosing the right Polyester Fiber is a commercial decision, not a simple material comparison. The wrong grade can cause pilling, weak seams, uneven dyeing, or costly production delays. A buyer may see similar white fibers in two bags. Their performance can differ sharply after spinning, finishing, and repeated washing. That gap matters.
A reliable selection process connects end use, process conditions, quality targets, and total cost. Apparel, home textiles, automotive fabrics, and nonwovens demand different fiber properties. Staple length, denier, crimp, strength, shrinkage, and finish all influence the final result. Recycled content may support sustainability goals, but it can affect consistency and color control. Ask for test reports, batch data, traceability records, and clear technical specifications. Supplier certificates help, yet they do not replace independent verification. Small samples reveal more than polished sales claims.
This guide explains how to compare fiber types against real production needs. It considers virgin and recycled options, applications, processing behavior, and supplier reliability. A practical trial should measure softness, tensile performance, dye uptake, and dimensional stability under your own conditions. Do not choose the lowest price too quickly. A cheaper fiber can increase waste, downtime, and customer complaints. Even experienced teams can miss one variable. That is worth remembering. With disciplined testing and honest review, businesses can choose Polyester Fiber with greater confidence and fewer surprises.
Define PET Requirements: 1.38 g/cm³ Density and 0.4% Moisture Regain
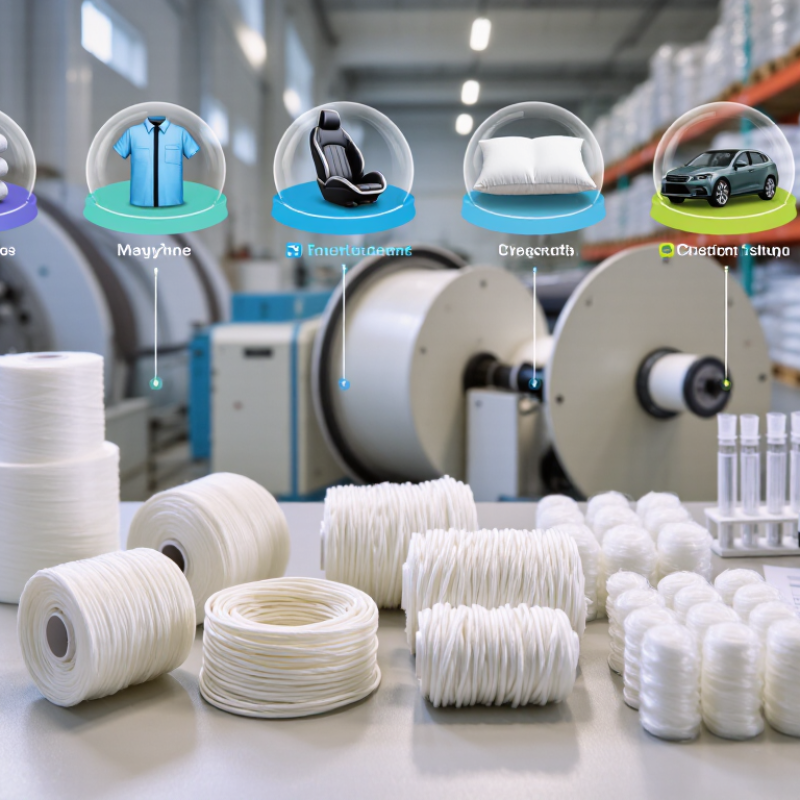
Choosing the right polyester fiber starts with a measurable PET specification. Textile Exchange’s Materials Market Report 2024 states that polyester represented about 57% of global fiber production in 2023. This scale makes consistent quality essential for apparel, filling, and industrial textiles. A practical starting point is a density near 1.38 g/cm³, commonly associated with PET fiber. Check the supplier’s technical sheet and verify the value through laboratory testing.
Moisture regain deserves equal attention.
Polyester typically shows about 0.4% moisture regain under standard conditioning, according to widely used textile testing references, including ASTM-based procedures. This low figure supports quick drying and stable dimensions. It can also increase static buildup during carding, weaving, or garment cutting. In production trials, measure moisture before opening bales. A damp warehouse floor can distort the result.
Do not treat 1.38 g/cm³ and 0.4% as universal guarantees.
Fiber shape, finish, draw ratio, and test temperature may change performance. ASTM D629 and related conditioning practices can help laboratories compare samples consistently. Ask for test conditions, not only headline numbers. That small detail matters. I have seen fibers pass a basic specification yet behave differently on high-speed equipment. The overlooked issue was finish uniformity. A repeat test is often cheaper than a failed production lot. Textile Exchange’s market data supports polyester’s importance, but operational evidence should guide the final purchase.
Match Denier and Cross-Section to End-Use Performance Needs
How to Choose the Right Polyester Fiber for Your Business?
Match Denier and Cross-Section to End-Use Performance Needs
Denier controls the fiber’s linear density, handle, coverage, and processing behavior. Finer fibers can create softer fabrics with better drape. Coarser fibers usually provide stronger bulk and improved resilience. The correct choice depends on the product, not simply the lowest price. For lightweight apparel, fine denier may improve comfort and surface smoothness. For filling materials, heavier denier can deliver loft and recovery under repeated compression. Small changes matter.
Cross-section adds another performance lever. Round fibers often process predictably and provide balanced strength. Hollow fibers can increase insulation and reduce weight. Trilobal or other shaped profiles may improve luster, wicking, or surface coverage. However, these benefits can change after spinning, finishing, and washing. A profile that performs well in testing may behave differently on a high-speed production line.
Use actual end-use trials before approving a specification. Check tensile strength, crimp recovery, moisture movement, abrasion resistance, and fabric appearance. Compare results after laundering or repeated compression. Measure twice. Our production experience shows that denier and cross-section must be evaluated together. A fine, hollow fiber may feel excellent but lack process stability. A shaped fiber may improve coverage yet create unwanted shine. I have also seen teams trust supplier data too quickly. Lab results are useful, but they never replace controlled sampling, operator feedback, and honest review of production losses.
Verify Strength and Elongation Under ISO 2062 Test Methods
How to Choose the Right Polyester Fiber for Your Business?
Polyester fiber selection should begin with measurable performance, not appearance alone. ISO 2062 provides a controlled method for testing yarn breaking force and elongation at break. These values show how the material may behave during weaving, knitting, sewing, or further processing. A strong yarn can still perform poorly if its elongation is unsuitable. Excessive stretch may distort fabric dimensions, while limited elongation can increase breakage during high-speed production. Request the test report, but examine the details. Check gauge length, pretension, extension rate, conditioning atmosphere, and the number of specimens tested. Without these details, comparisons may be unreliable. Small testing differences can change purchasing decisions.
Tips: Compare samples from several production lots. Ask for average values and variation, not only the best result. Confirm that testing follows the current ISO 2062 procedure and uses calibrated equipment. A practical trial is also valuable. Run the yarn through your actual machine and record breaks, tension changes, and surface defects. Laboratory data matters. Factory behavior matters too. One weakness in procurement is trusting a single result. Another is ignoring humidity and storage conditions. Polyester is stable, but processing conditions still influence handling and measurement. Review failures honestly, even when the report looks acceptable. That reflection may reveal a better specification for your business.
Compare Recycled Content and Traceability Using Textile Exchange Data
Choosing polyester starts with evidence, not the recycled label. Textile Exchange data provides a useful market baseline: recycled polyester remains a minority of total polyester production, while fossil-based virgin polyester still dominates. This gap matters when a product team sets a recycled-content target. A high percentage on one style does not prove broad supply-chain progress. Define the target by weight, product, and season. Keep it measurable.
Then test traceability. Ask where the polymer was produced, how feedstock was collected, and whether mass balance or physical segregation applies. Textile Exchange guidance and chain-of-custody data help distinguish these routes. Physical segregation can offer clearer material identity. Mass balance may improve scale, but it requires careful claims. Request transaction records, scope documents, and independent certification. Do not accept a polished spreadsheet as proof. Too simple.
In supplier reviews, compare three figures: recycled input, certified output, and unexplained loss. The numbers should connect across purchase orders, production batches, and shipping records. For bottle-based polyester, ask whether collection data supports the claimed origin. For textile-to-textile inputs, examine sorting and chemical or mechanical processing details. Textile Exchange reports are valuable, but they cannot replace supplier-level verification. Data definitions can shift between editions. That deserves attention. A lower recycled percentage with strong traceability may be more credible than a larger claim with weak evidence. Review the choice after washing tests, dyeing trials, and cost checks. Performance still matters.